


Technical library
Open dies, impression dies and rolled rings solve different geometry and production questions.
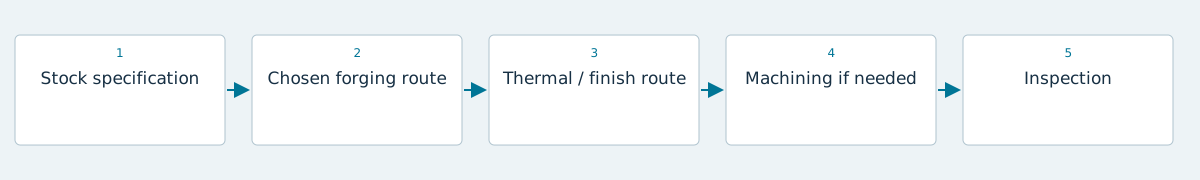
Three route families
The Aluminum Association describes open-die, impression-die and rolled-ring forging. Open dies allow freer deformation; shaped impression dies constrain the metal into more defined geometry; rolled rings use a ring preform. These distinctions support an initial supplier discussion, but the drawing, production quantity and acceptance specification must establish which route is appropriate.
Describe the purchased state
Decide whether the enquiry concerns a forging blank, a partly machined forging or a finished component. Show machining allowances and identify which surfaces establish datums. Ask the producer to propose the route, alloy and delivered condition against the actual functional requirements. A supplier capability statement does not by itself prove that a particular part meets them.
Connect inspection to function
Request an inspection proposal for the features that matter to service. Clarify dimensional checks, material testing and any specified internal examination, including their acceptance basis. Ask how test material represents the supplied forging and how identification survives machining. Do not replace this project-specific plan with a general assertion that forged aluminium is always stronger than another route.
Compare the complete offer
Review tooling, minimum order, material documentation, machining, finish and approval samples alongside the unit price. Establish how drawing or process changes affect the qualified product and who approves substitutions. Qualification requirements depend on the application and governing specification. This overview intentionally avoids forging temperatures, universal fatigue values and guarantees based only on manufacturing method.
Continue exploring
Alloy database · Product guides · Engineering calculators
Sources and verification
Selected facts checked 14 October 2026. Source data is reference information, not certification of supplied material.
- Aluminum Association • Processing 101 — Live public page; no publication revision stated · checked 2026-10-14
Separate feedstock approval from finished-forging inspection
Casting and heat-treatment equipment serve different stages of the forging route. Define stock preparation and charge dimensions with the forger, then retain finished geometry, grain-flow and inspection requirements in the component programme. Raw-stock chemistry, initial charge mass and final machined condition answer different questions and should not share an undifferentiated certificate.
Source: www.gautschi.cc, www.aluminum.org





