


Technical library
DC casting research illustrates why alloy, geometry and validated operating conditions must stay together.
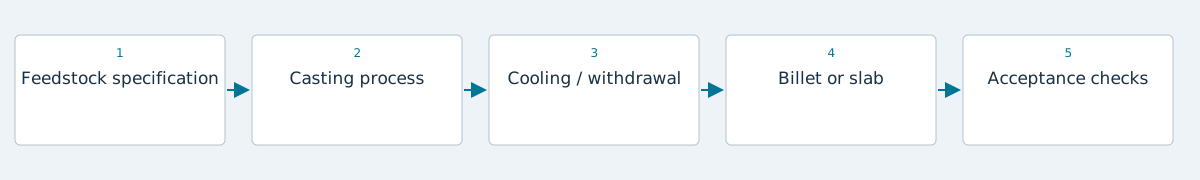
Understand the evidence
The Waterloo repository describes laboratory work on conventional direct chill casting and a subsequent co-casting development. DC casting is a feedstock-manufacturing subject, distinct from machining a finished part. The cited research concerns specific alloys and a laboratory caster; its abstract is useful evidence about the variables studied, not a production recipe for an industrial casthouse.
Cooling is a system
The experiments examined casting speed, water flow and melt superheat using thermal-history and sump measurements. The reported results were sensitive to casting speed. The practical lesson for a procurement review is to ask how the proposed alloy and section are qualified, rather than assuming one published setting can be transferred to another caster or ingot geometry.
Ask about the supplied condition
Identify whether the purchase concerns extrusion billet, rolling slab or another feedstock form. Ask the producer to state chemistry, identification, dimensions, surface requirements and any downstream preparation included in supply. Keep proposed homogenization or other treatment requirements tied to the actual alloy and purchase specification. Do not infer an ingot’s acceptance from the name of its casting technology.
Model validation and acceptance differ
A thermal model can support process development, while shipment acceptance needs agreed inspection and documentation. Ask what production evidence connects development work to the offered feedstock and how deviations are handled. Only the public thesis abstract was reviewed here. Its laboratory findings should not be generalized into casting-speed limits, cooling-water settings or guaranteed industrial quality.
Continue exploring
Alloy database · Product guides · Engineering calculators
Sources and verification
Selected facts checked 14 October 2026. Source data is reference information, not certification of supplied material.
- University of Waterloo • Direct Chill Casting of Aluminum Alloys: Experimental Methods and Design — Harry Ng, 2011; repository abstract read, full thesis not read · checked 2026-10-14
Qualify the output around its downstream mill
Wagstaff distinguishes billet and rolling-ingot casting, and Gautschi identifies casting equipment for slab, billet, forging stock and foundry ingot. These outputs have different downstream routes. Agree chemistry, preparation, lot identification and inspection with the receiving extruder, roller or forger. A casting-control description is not itself a finished-profile or sheet certificate.
Source: www.wagstaff.com, www.gautschi.cc





