


Technical library
Machine capability matters only when it connects to the component drawing and acceptance method.
What the manufacturer demonstrates
Kersten describes five-axis machining of straight and bent aluminium profiles, including complex cut-outs and weld preparation. That example establishes a practical manufacturing route for shaped profiles. It does not establish a universal tolerance or show that every shop can hold the same features on every alloy, length and wall thickness.
Create a usable drawing
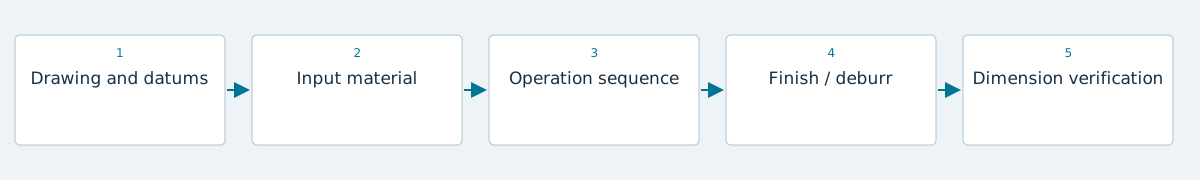
Identify datums, critical fits, thread requirements and the functional surfaces that matter to the assembly. Provide a controlled model and drawing revision, and resolve which document governs when they differ. Ask the machinist to identify inaccessible features or proposed changes before ordering. The enquiry should communicate the required component outcome rather than prescribe unexplained tool choices.
Agree the operation sequence
Describe whether the input is plate, bar, extrusion, casting or forging, and state its supplied condition. Identify subsequent welding, bending and surface treatment. Clarify whether dimensional acceptance occurs before or after those steps and whether the final inspection checks the assembled state. A dimension achieved during machining may not be the only dimension relevant to the finished product.
Verify what was delivered
Request an inspection plan naming the critical features, measurement basis and reporting requirements. Agree deburring, cleanliness, edge treatment and packing where they affect use. Supplier-specific machine capacities are useful screening information; confirm current capacity against the actual part instead of generalizing a published machine envelope. Cutting speeds, tooling recipes and performance guarantees require a qualified production plan.
Continue exploring
Alloy database · Product guides · Engineering calculators
Sources and verification
Selected facts checked 14 October 2026. Source data is reference information, not certification of supplied material.
- Kersten • Five-axis machining — Live public page; no publication revision stated · checked 2026-10-14
Specify stability after planned metal removal
AMAG and UACJ treat stability and residual stress as concerns independent of strength. Deep pockets, one-sided removal and thin walls can make a final part’s geometry the important acceptance condition. Supply the machining plan, final datum and measurement setup; as-delivered plate precision does not define the final fixture result.
Source: www.amag-al4u.com, www.uacj.co.jp





